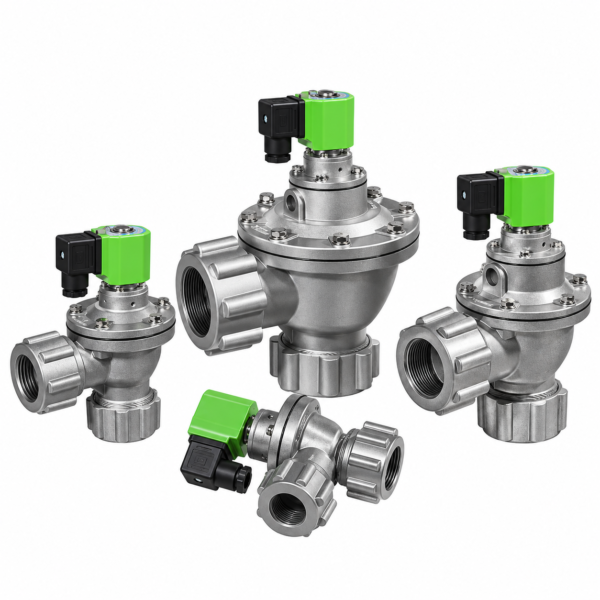
Right-Angle Quick-Connect Pulse Solenoid Valve features an external threaded quick-connect design for faster installation and replacement. Its 90° inlet and outlet configuration provides smooth airflow and a compact installation structure. Installed externally on the air reservoir, it supports reliable pulse cleaning and works with pulse controllers, differential pressure controllers, and automatic control systems.
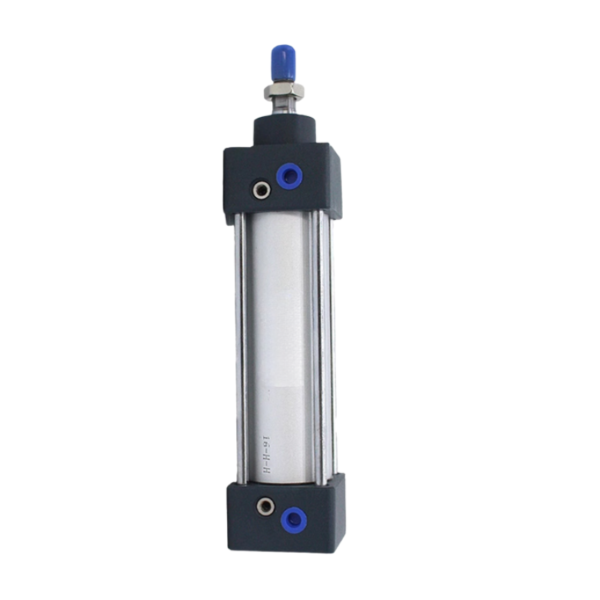
Pneumatic Cylinder is a pneumatic actuator that uses compressed air to generate linear motion. It is widely used in automation equipment and dust collection and powder handling systems to drive material gates, dampers, discharge mechanisms, and other components requiring linear movement.
Pneumatic Vibrator uses compressed air to generate high-frequency vibration, helping reduce material adhesion, buildup, bridging, and blockage. It is suitable for dust collector hoppers, silos, chutes, powder conveying pipelines, and bulk material handling equipment. Different models can be selected according to equipment structure, material characteristics, and required vibration force.
Pneumatic Percussion Hammer, also known as an air hammer or pneumatic piston vibrator, uses compressed air to drive an internal piston and generate powerful linear impact force.
It effectively helps prevent material adhesion, buildup, blockages, and bridging during powder handling and storage, ensuring smooth material discharge from hoppers and pipelines.
It is widely used in the chemical, cement, pharmaceutical, and food industries, including powder silos, hoppers, and dust collector systems, and is suitable for many dusty or humid operating environments.
Dust Detection Alarm provides real-time dust concentration monitoring for industrial environments and dust collection systems. Based on laser scattering technology, it monitors PM2.5, PM10, and airborne dust concentrations. With 4–20 mA, RS485, and switch signal outputs, it can integrate with PLC, DCS, alarm systems, and other industrial control equipment.
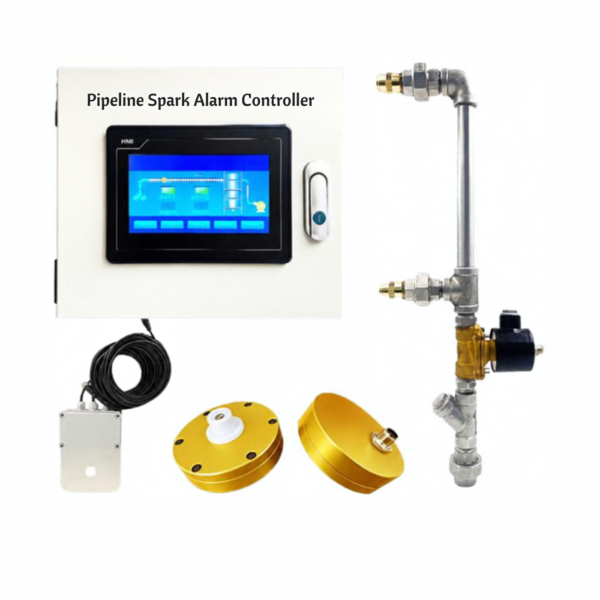
Pipeline Spark Detection & Alarm System provides early detection of sparks, embers, and hot particles traveling through industrial dust collection and conveying ducts. The system can integrate spark detection, audible and visual alarms, extinguishing, and safety interlocking to help prevent ignition sources from reaching downstream dust collectors, filters, and other critical equipment.
We use essential cookies to make our site work. With your consent, we may also use non-essential cookies to improve user experience and analyze website traffic.
By clicking “Accept,” you agree to our website's cookie use as described in our Cookie Policy.
You can change your cookie settings at any time by clicking “Preferences.”