1. Features & Functions
High-Efficiency Vibration to Reduce Blockage
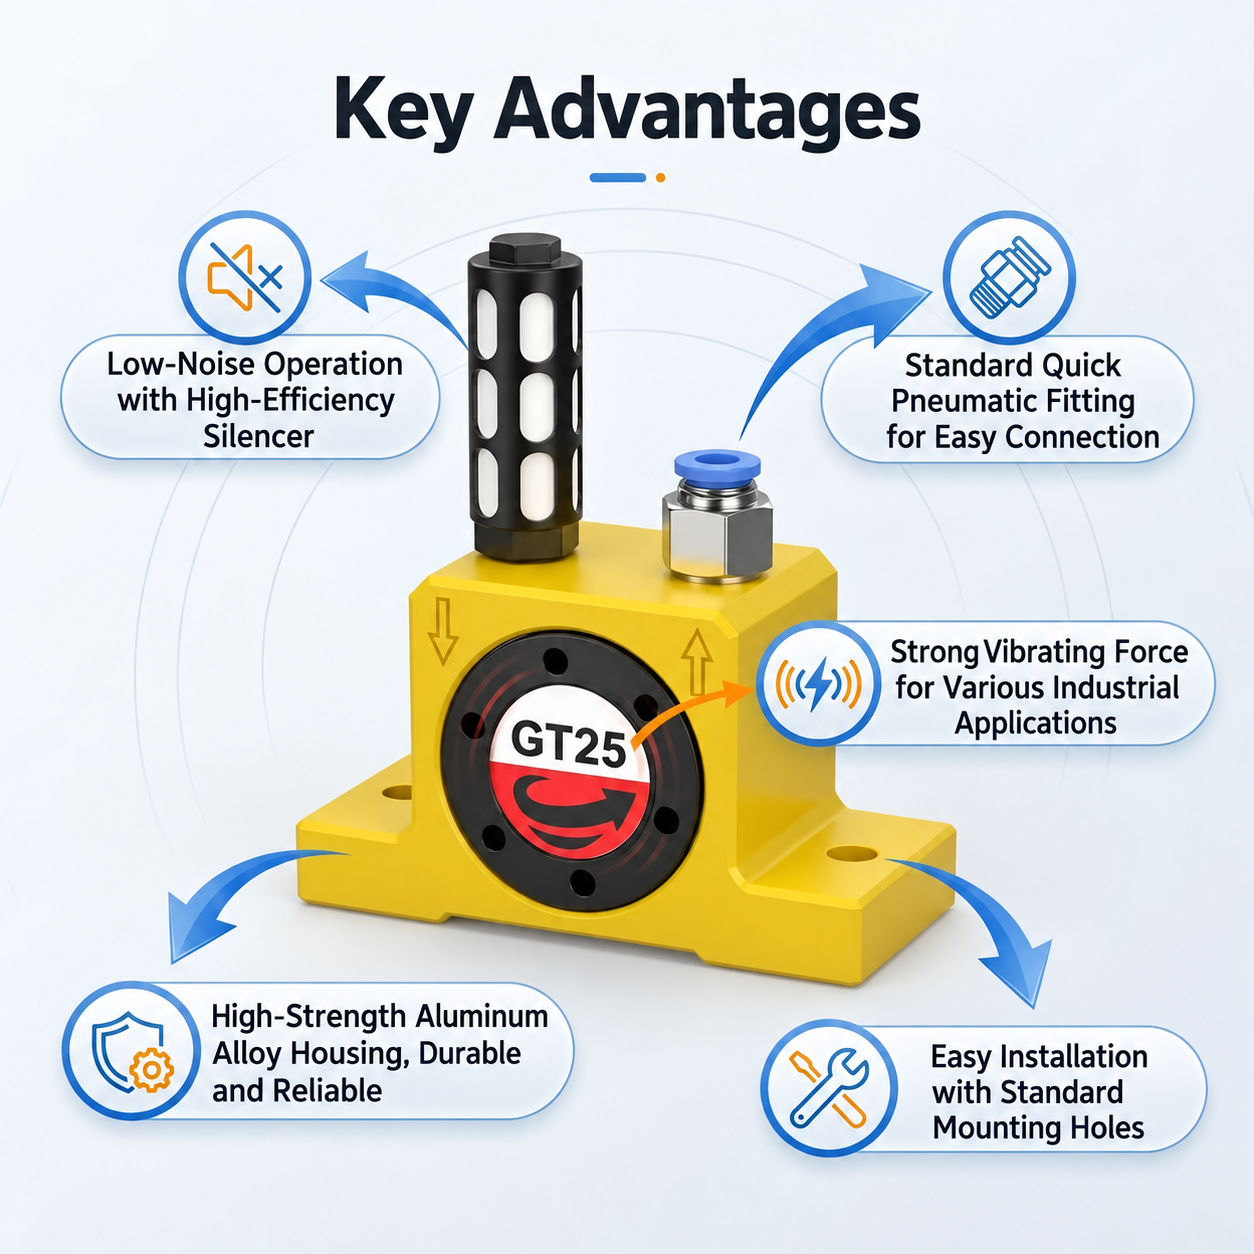
Driven by compressed air, the internal vibration mechanism generates vibration to loosen material adhesion and buildup, helping reduce powder bridging and blockage and improving material discharge from hoppers, dust collector hoppers, and silos. The vibration intensity and frequency can be adjusted according to operating conditions.
Adjustable Vibration Force
By adjusting the compressed air pressure, the operating frequency and vibration force can be changed to suit different materials and installation positions. Different models cover different vibration force ranges, making it easier to select the appropriate vibrator for specific equipment.
Fast Start and Stop
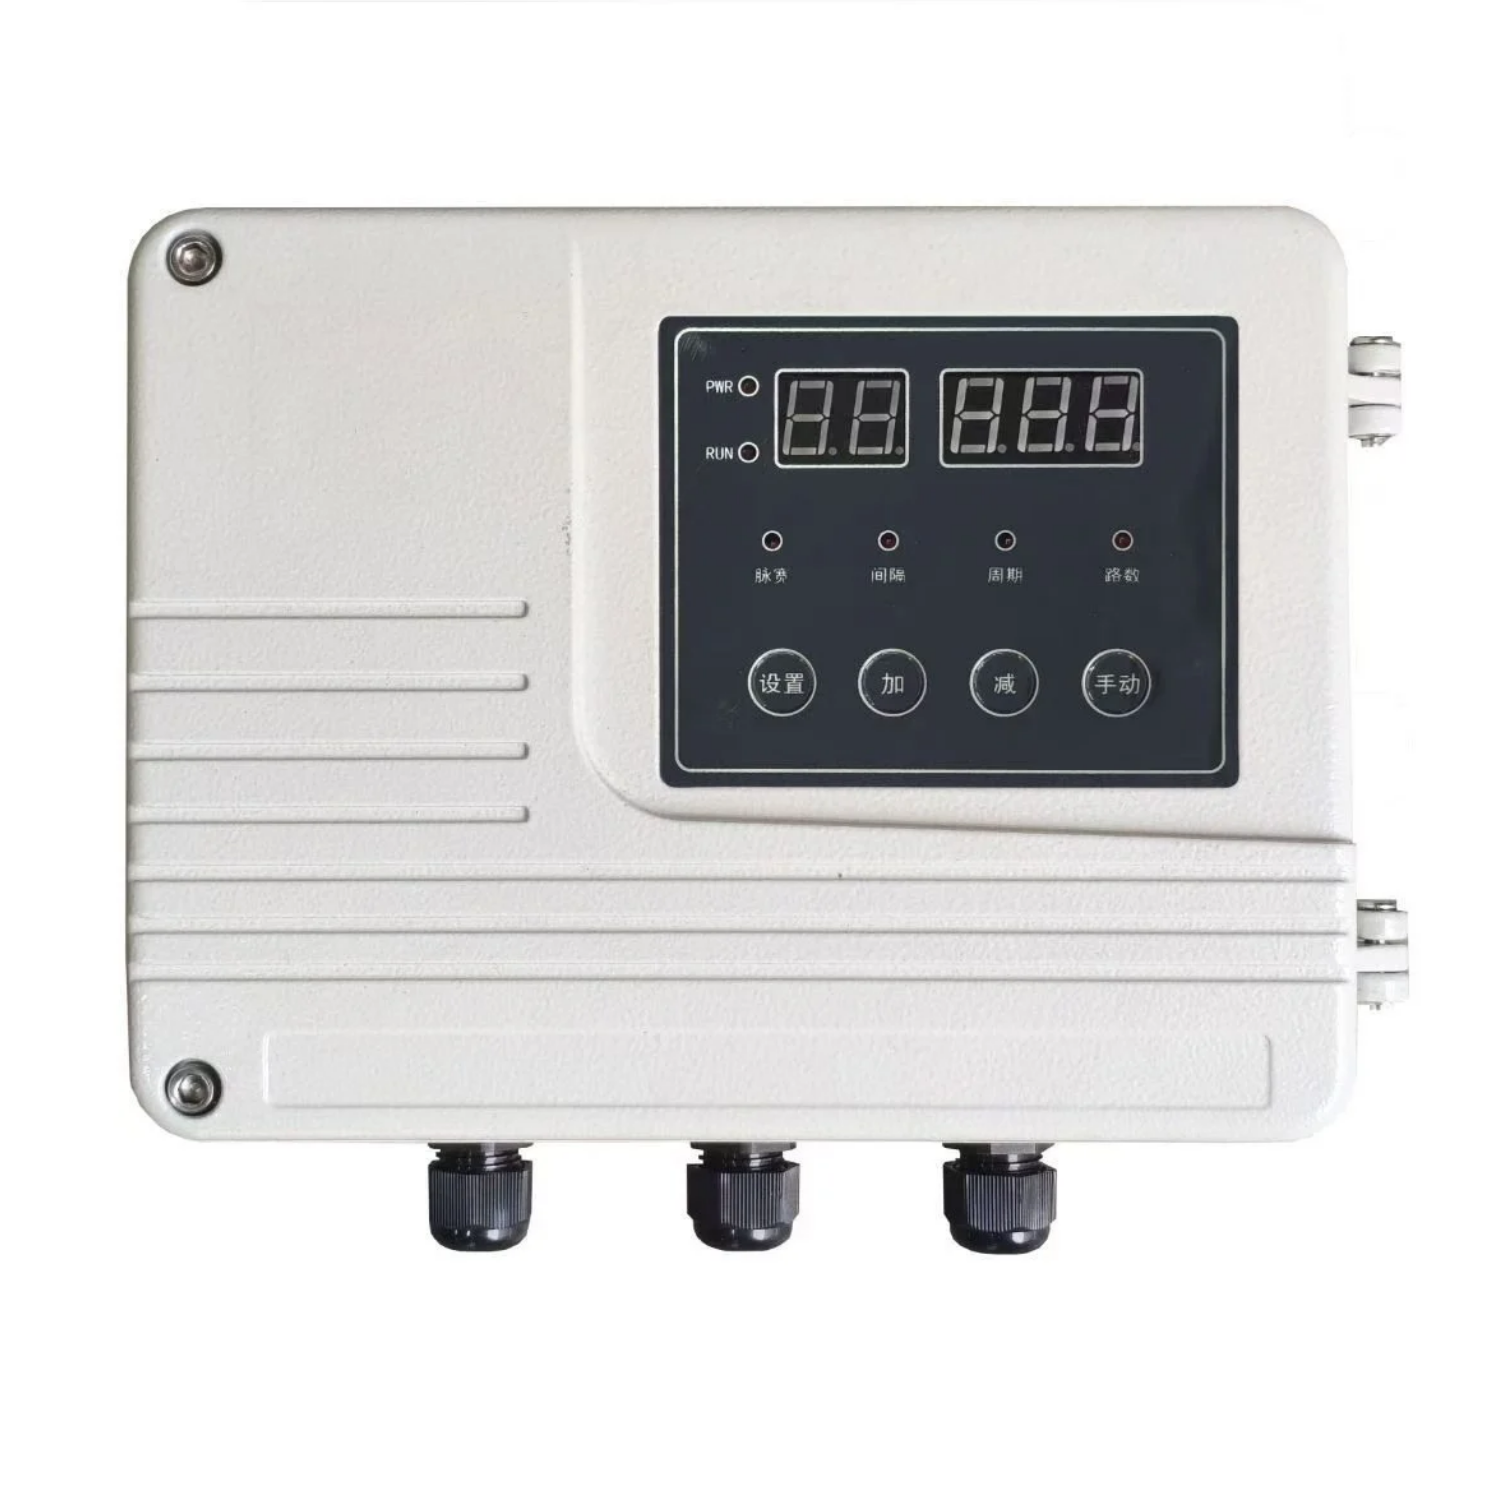
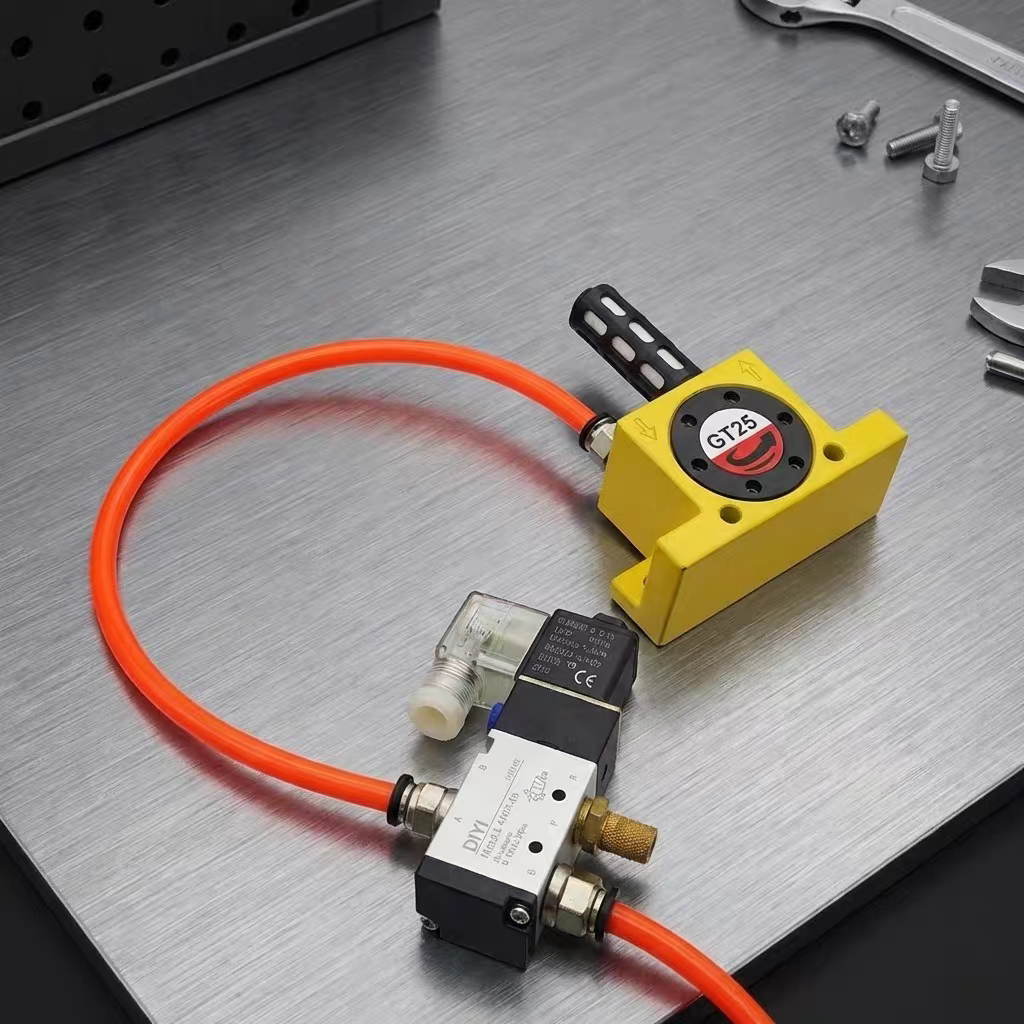
The Pneumatic Vibrator is driven by compressed air and can start and stop quickly. It is suitable for use with solenoid valves, timers, pulse controllers, or PLCs to achieve automatic intermittent vibration.
Compact Design and Easy Installation
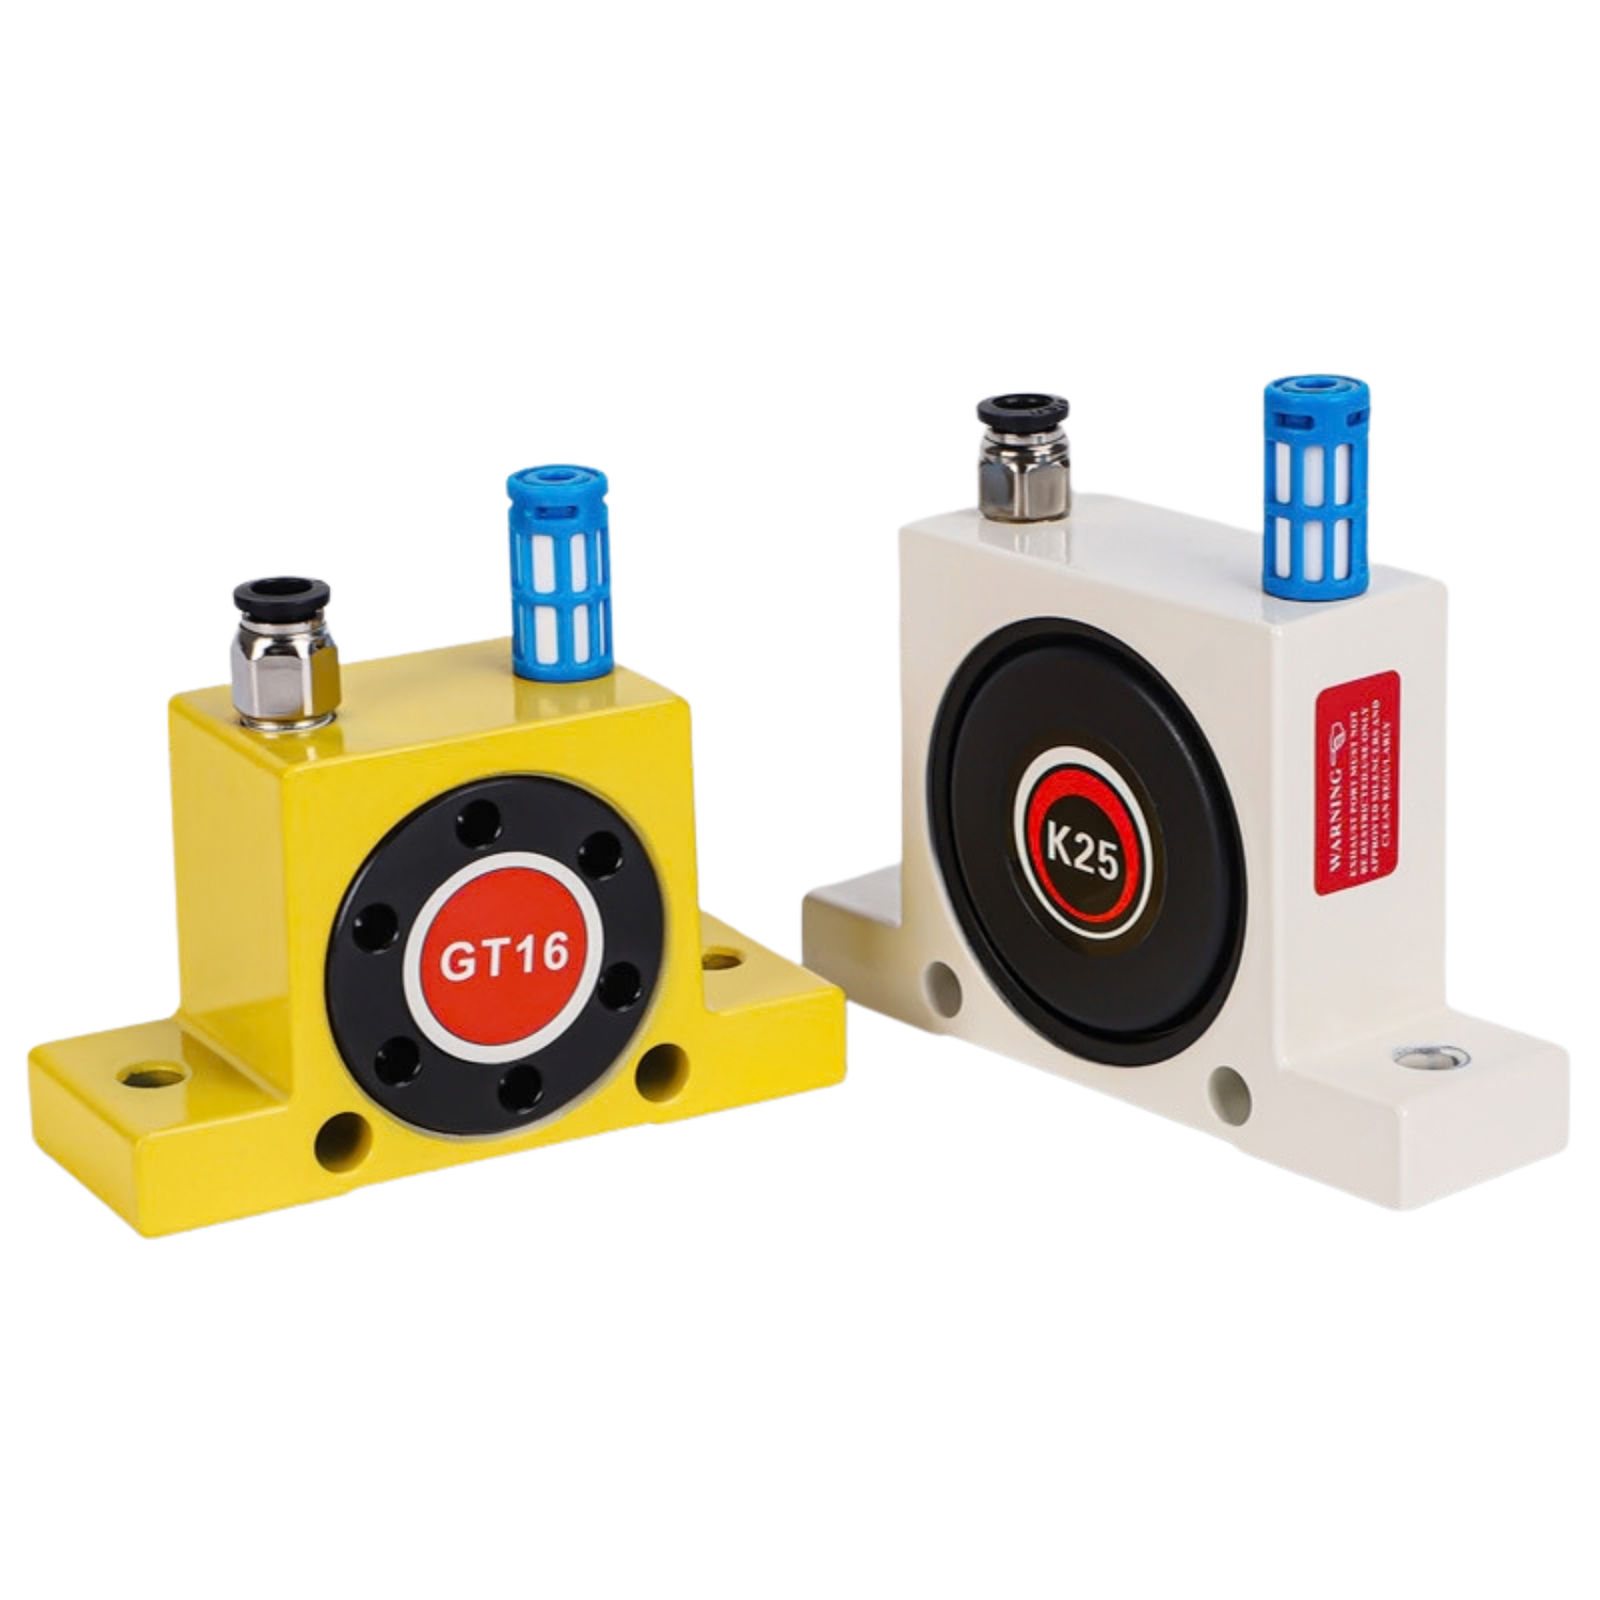
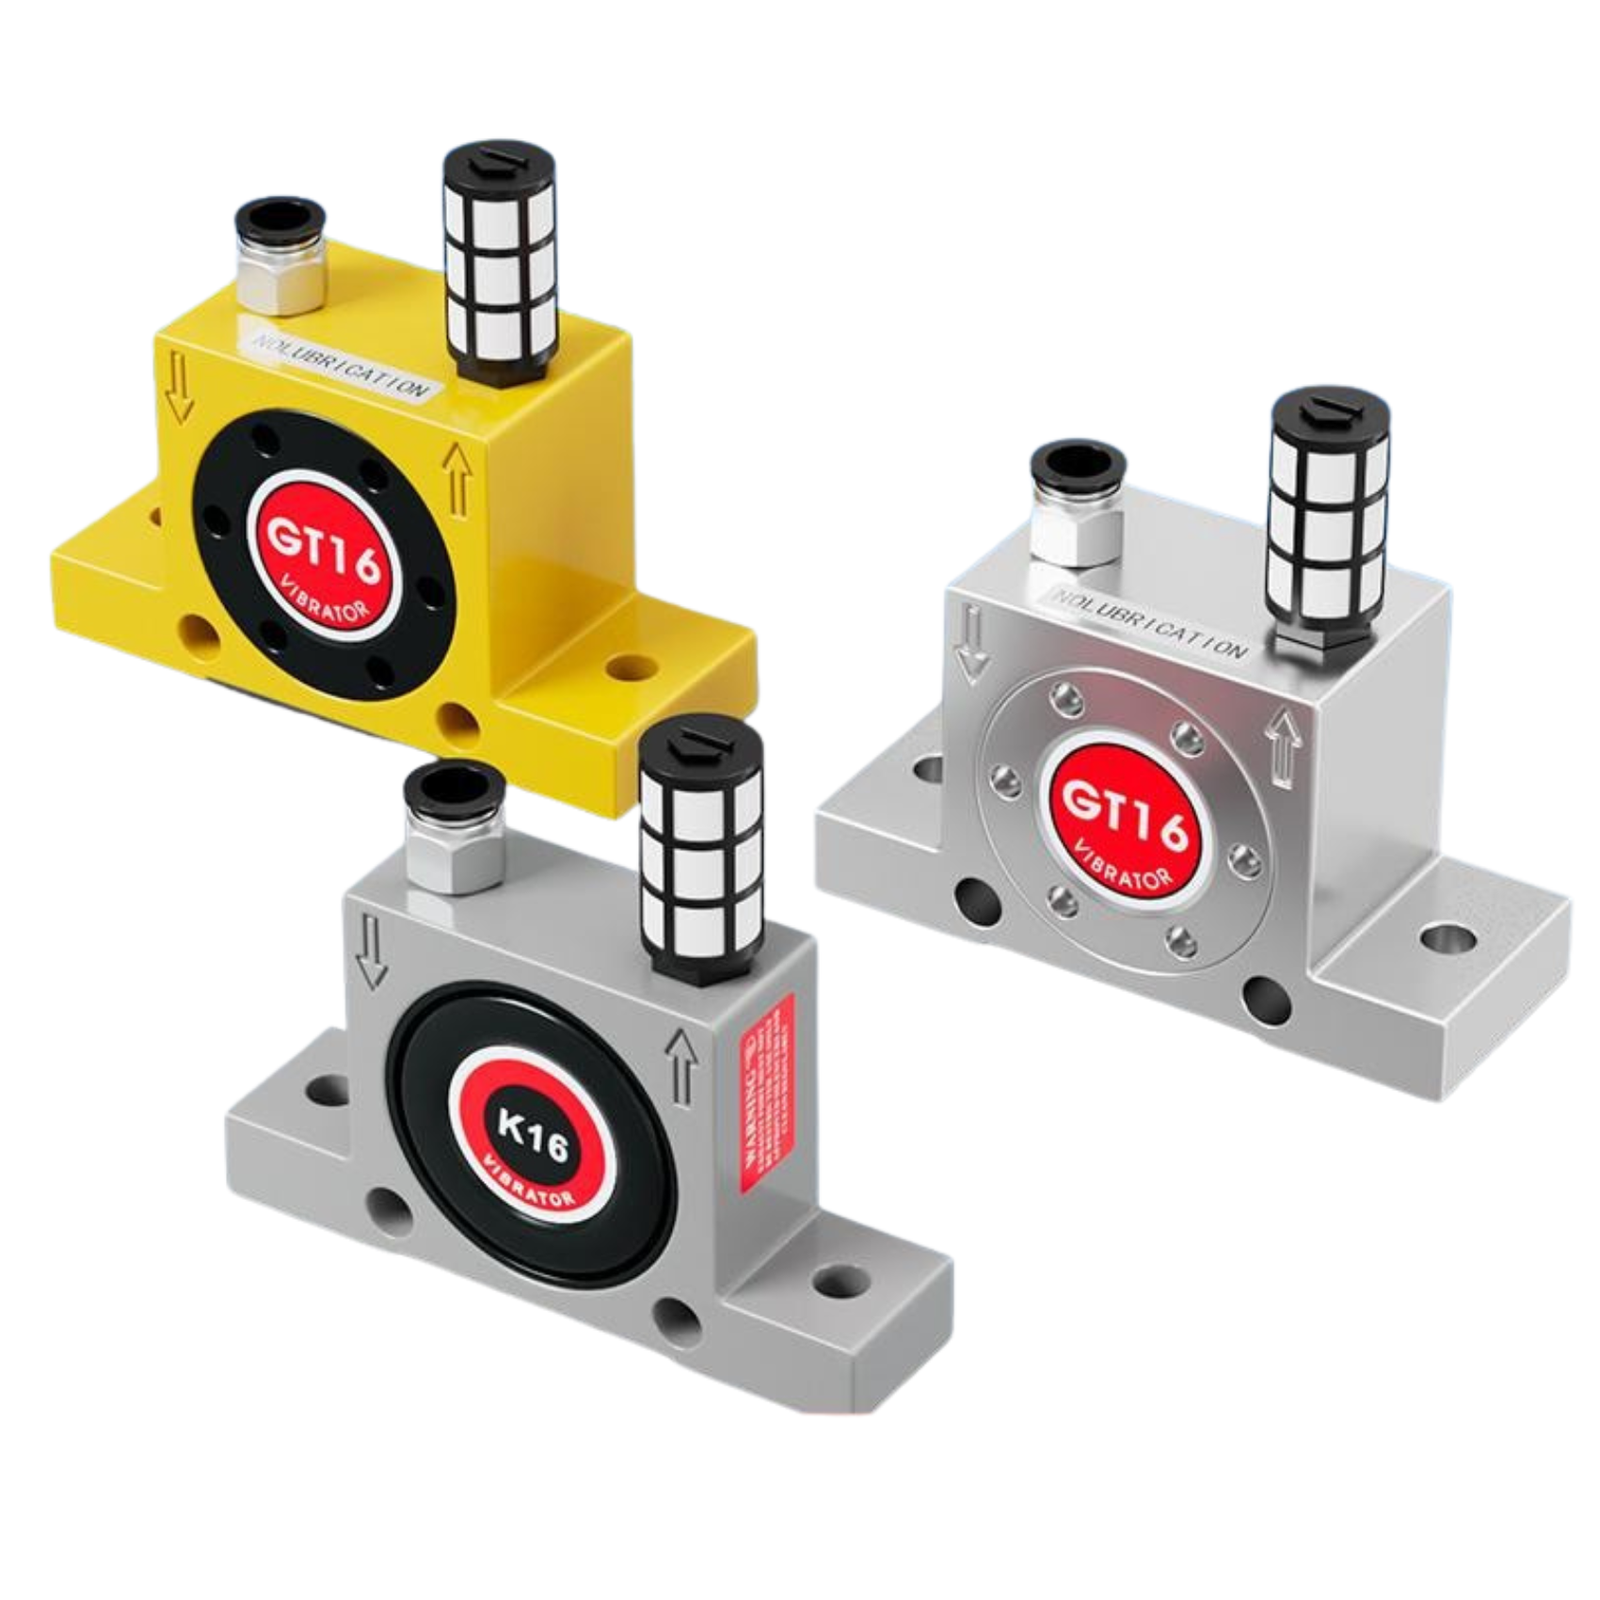
The product features a compact design and can be mounted to the walls of hoppers, silos, or other equipment through mounting holes. Different series and specifications are available to suit various installation spaces and vibration force requirements.
Multiple Models Available
Different types of Pneumatic Vibrators can be selected according to the vibration principle and application requirements, covering different levels of vibration force, frequency, and air consumption.
2. Typical Applications
Pneumatic Vibrators can be used in a wide range of industrial powder and bulk material handling equipment:
- Dust Collector Hoppers
- Hoppers
- Silos
- Bins
- Chutes
- Powder Conveying Systems
- Pneumatic Conveying Systems
- Screw Conveyors
- Feeders
- Powder Processing Equipment